Multi Purpose Pilot Plant Unit
Goel Glass manufactures turnkey Multipurpose Glass Pilot Plant Units engineered specifically for pharmaceutical R&D, biotechnology laboratories, and specialty chemical manufacturers. Designed for versatile operational scale-up, kinetic simulation, and cGMP kilo-lab production, these modular units empower chemists and chemical engineers to perform complex synthesis, liquid dosing, multi-stage chemical reactions, atmospheric or vacuum distillation, phase separation, and solvent recovery within a single skid-mounted envelope.
Constructed entirely from premium Borosilicate Glass 3.3 and virgin PTFE wetted contact components, the multi-purpose system delivers unmatched corrosion resistance against highly aggressive reagents, mineral acids, and organic solvents while maintaining full 360-degree process visibility. Each system is supported by a rigid stainless steel (SS304/SS316) or epoxy-coated structural tubular framework engineered for vibration dampening and cleanroom compatibility.
System Capabilities & Features :
- Jacketed full glass reactor, cylindrical vessel with heating bath, or spherical flask options
- Multipurpose glass overhead assembly with reflux divider, primary condenser, and sub-cooler
- Rigid stainless steel (SS304/SS316) or powder-coated tubular support structure
- ATEX / Flameproof or Non-flameproof electrical drives with variable speed control
- Full vacuum operation down to 1 mbar and operational thermal range from -50°C to +200°C
- Integrated PT-100 temperature sensors with digital indication and automated PID control
- Multi-port glass cover for solid charging, nitrogen inerting, liquid feed, and sampling
- Corrosion-resistant PTFE bottom flush-outlet drain valve with zero dead volume
- Dual calibrated receiver flasks for continuous fraction collection without breaking vacuum
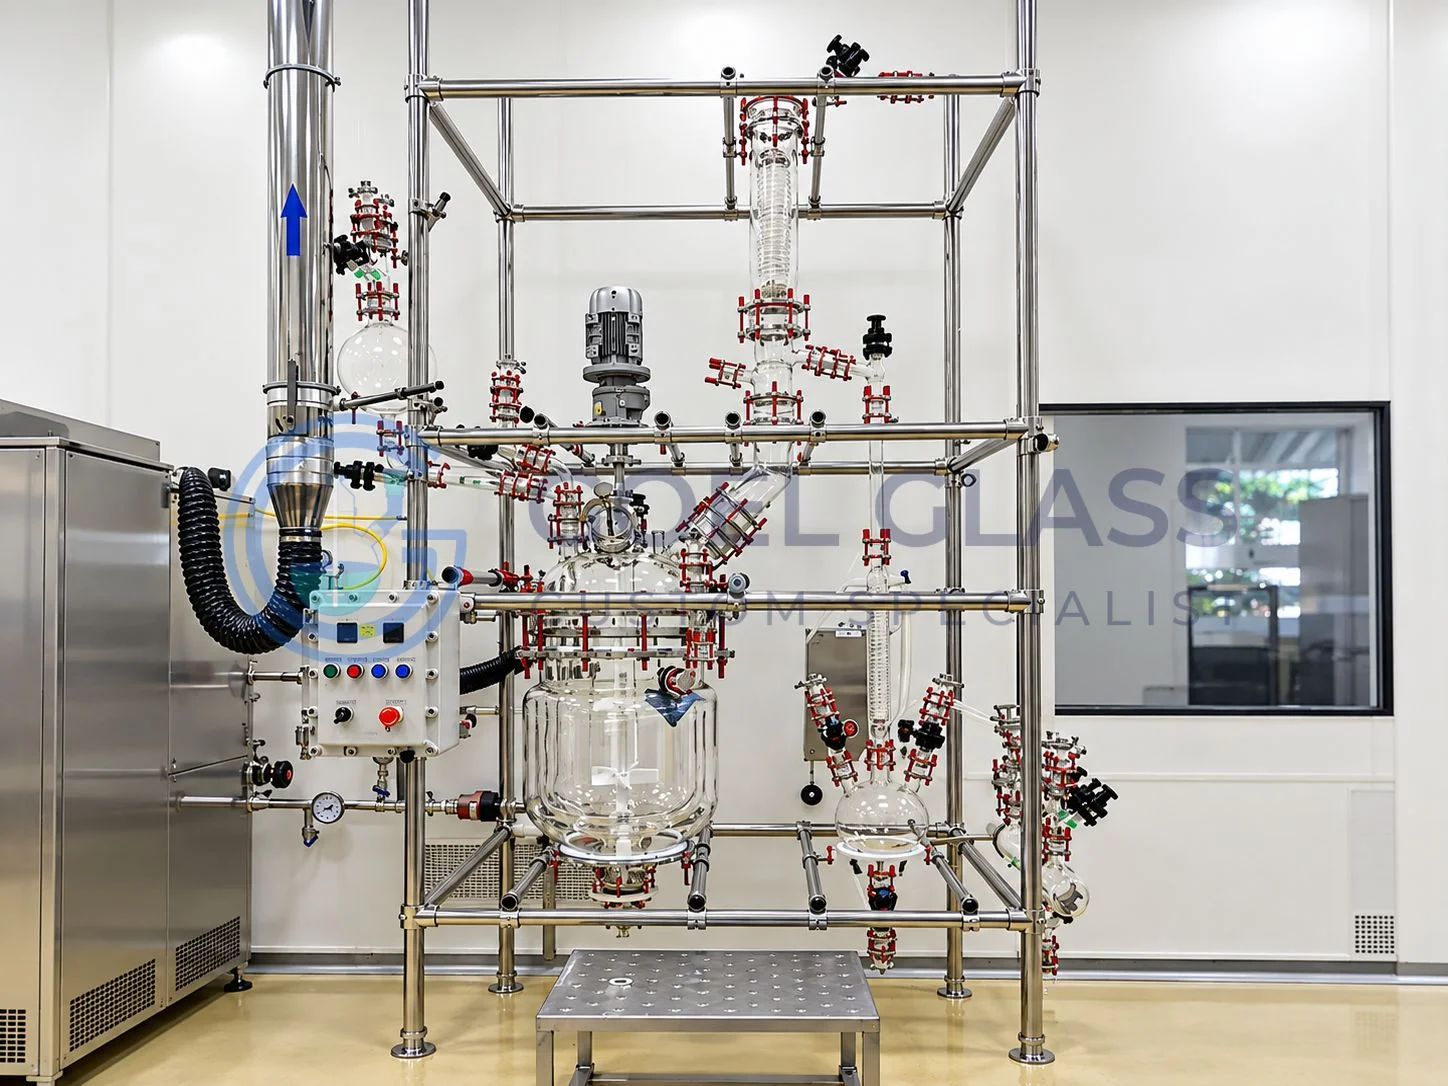
Key Engineering Features
- High-efficiency coil condensers for maximum vapor condensation and recovery
- PTFE stirrer shaft with interchangeable retreat-curve or pitch-blade turbines
- Magnetically operated reflux timer for automated liquid/vapor split ratios
- Sanitary mechanical seal providing vacuum integrity under continuous rotation
- Modular pipeline connections using Schott-style flat-butt or ball-socket joints
Industrial Applications
- Active Pharmaceutical Ingredient (API) scale-up and optimization
- Multi-step organic synthesis and high-purity chemical reactions
- Azeotropic and fractional distillation of heat-sensitive compounds
- Continuous solvent recovery and high-purity botanical extraction
- Process safety validation and kinetic reaction profiling in kilo labs
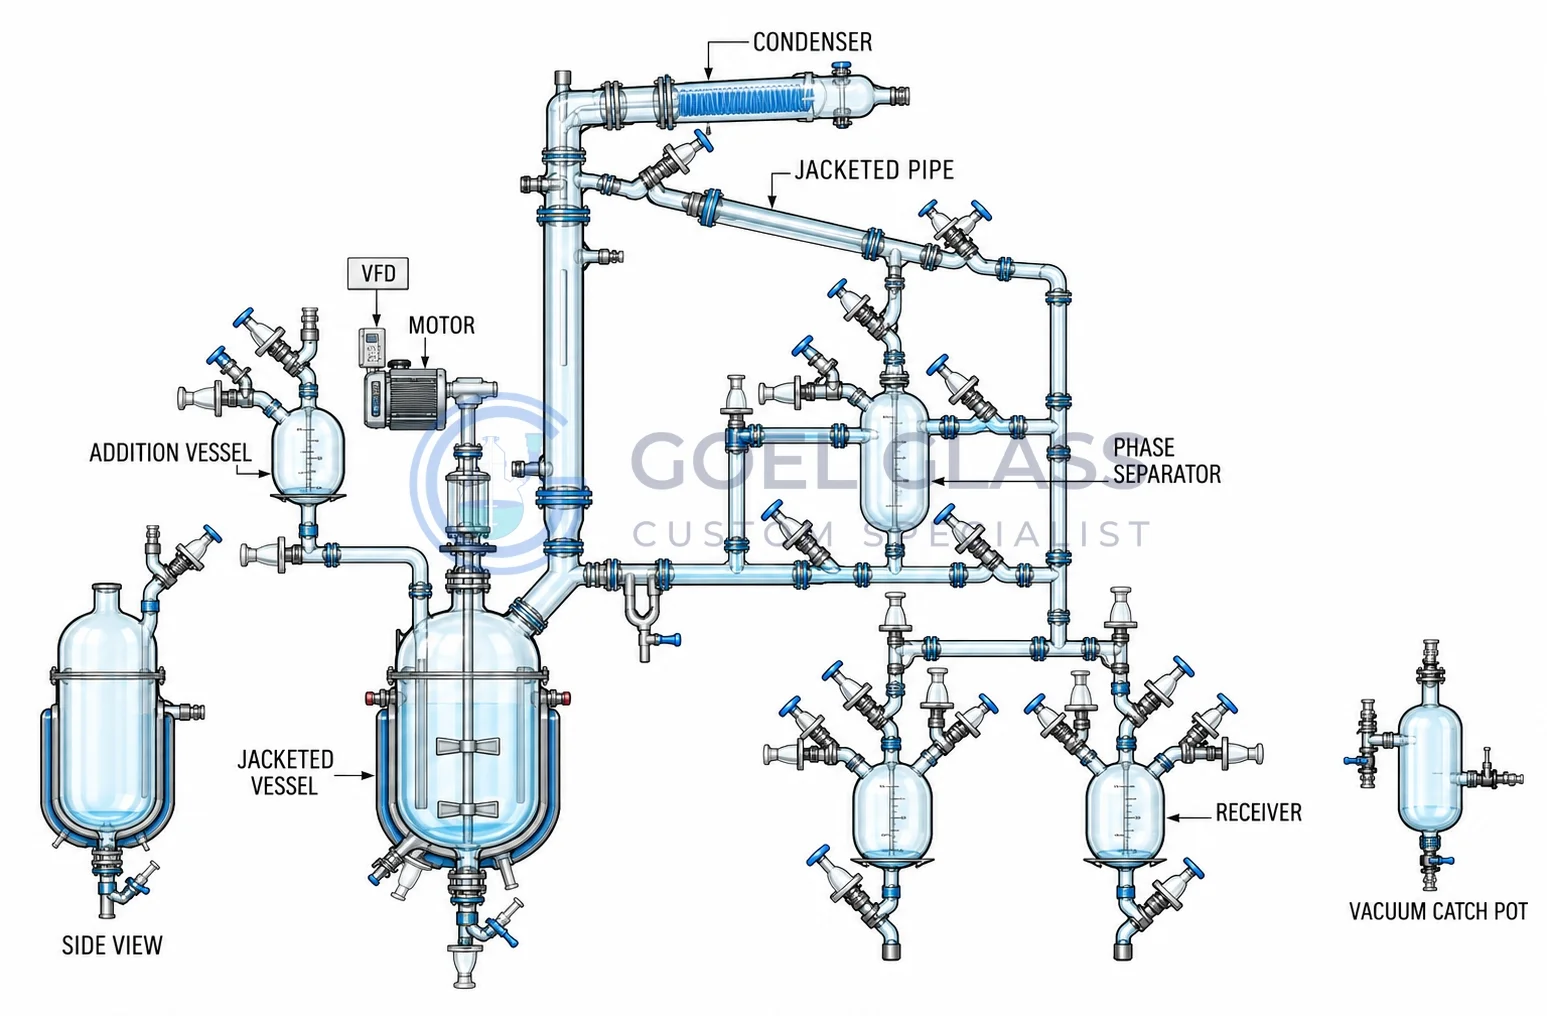
| Unit Cat.Ref. | Reactor Capacity | BATH KW | ADDITION VESSEL | VAPOUR LINE | CONDENSER HTA M2 | COOLER HTA M2 | RECEIVER SIZE |
|---|---|---|---|---|---|---|---|
| MPU20 | 20 L | 4.0 | 2 L | 80 DN | 0.35 | 0.10 | 2L, 5L |
| MPU50 | 50 L | 6.0 | 5 L | 100 DN | 0.50 | 0.20 | 5L, 10L |
| MPU100 | 100 L | 9.0 | 10 L | 150 DN | 1.50 | 0.35 | 10L, 20L |