Industrial Borosilicate Fractional Distillation Units
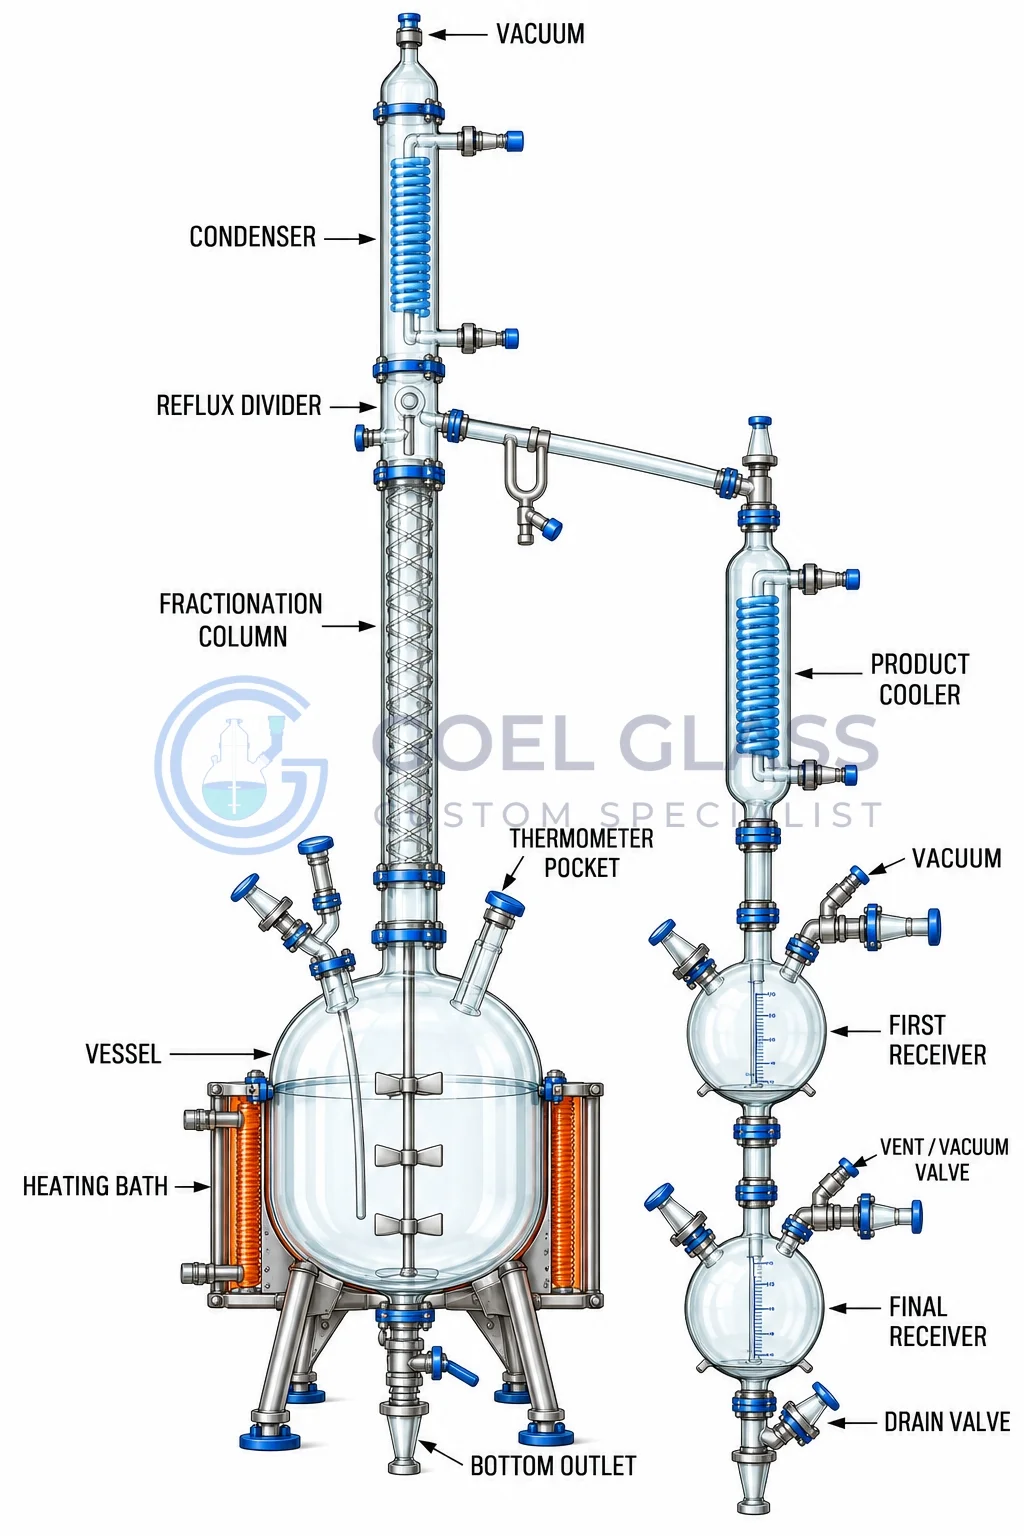
Goel Glass designs and builds skid-mounted Fractional Distillation Units engineered for high-efficiency multi-component chemical separations, solvent fractionation, and high-purity chemical purification. Each unit combines a Borosilicate 3.3 reboiler vessel seated in an electric heating bath with an overhead packed column section filled with high-surface-area borosilicate Raschig rings or structured packing to maximize theoretical plates.
Overhead process vapors enter an engineered reflux splitter assembly coupled with a primary coil condenser. Using a manual or magnetically actuated reflux divider with digital timer controls, the operator can adjust the reflux-to-distillate ratio from 100% total reflux to complete forward takeoff. Overhead distillate is passed through an auxiliary sub-cooler and directed into twin graduated receiver vessels with vacuum equalization lines, enabling continuous fractions sampling without breaking vacuum.
| Unit Cat.Ref. | Reactor Capacity | BATH KW | VAPOUR LINE | CONDENSER HTA M2 | COOLER HTA M2 | RECEIVER SIZE |
|---|---|---|---|---|---|---|
| FDU20 | 20 L | 4.0 | 80 DN | 0.35 | 0.10 | 2L, 5L |
| FDU50 | 50 L | 6.0 | 100 DN | 0.50 | 0.20 | 5L, 10L |
| FDU100 | 100 L | 9.0 | 150 DN | 1.50 | 0.35 | 10L, 20L |
Key Engineering Features
- Packed Fractionating Column: High free-volume column sections with optimized HETP for sharp separations.
- Precision Reflux Ratio Dividing: Magnetic or manual reflux splitters allow programmatic ratio adjustment.
- Full Vacuum Tightness: Certified for operation down to full vacuum (-1 bar) with zero-leakage PTFE joints.
- Twin Graduated Receivers: Dual collection vessels with vent & drain manifolds for uninterrupted fraction harvesting.
Industrial Applications
- Close-Boiling Solvent Separation: Purifying mixed solvent streams with narrow boiling point differentials.
- API & Intermediate Refining: Fine chemical crystallization precursor and intermediate batch concentration.
- Terpene & Essential Oil Fractionation: Thermal-stress-free distillation of delicate natural compounds under deep vacuum.
- Pilot Plant Scale-Up: Validation studies and process parameter optimization prior to large-scale column commissioning.